Conveying systems that keep production moving

We design and integrate custom conveying systems that connect processes, machines, and robotic cells into a continuous, reliable material flow, engineered to match your products, layout, and production requirements.

Where material flow becomes a bottleneck to production

When conveying systems are not designed around the product and the production process, material handling becomes inefficient, rigid, and costly. Poorly matched transport solutions disrupt flow, increase manual intervention, and limit the performance of the entire production line.

01

Rigid systems limit efficiency

Standard conveyors often fail to adapt to product characteristics or layout constraints.

02

Disconnected transport slows flow

Poor integration between machines, robots, and conveyors creates unnecessary stops and delays.

03

Manual handling increases strain

Inadequate conveying systems force operators to intervene more frequently.

04

Scaling becomes complex and costly

Systems not designed for growth require major rework when production increases.

Conveying systems engineered as part of the production system

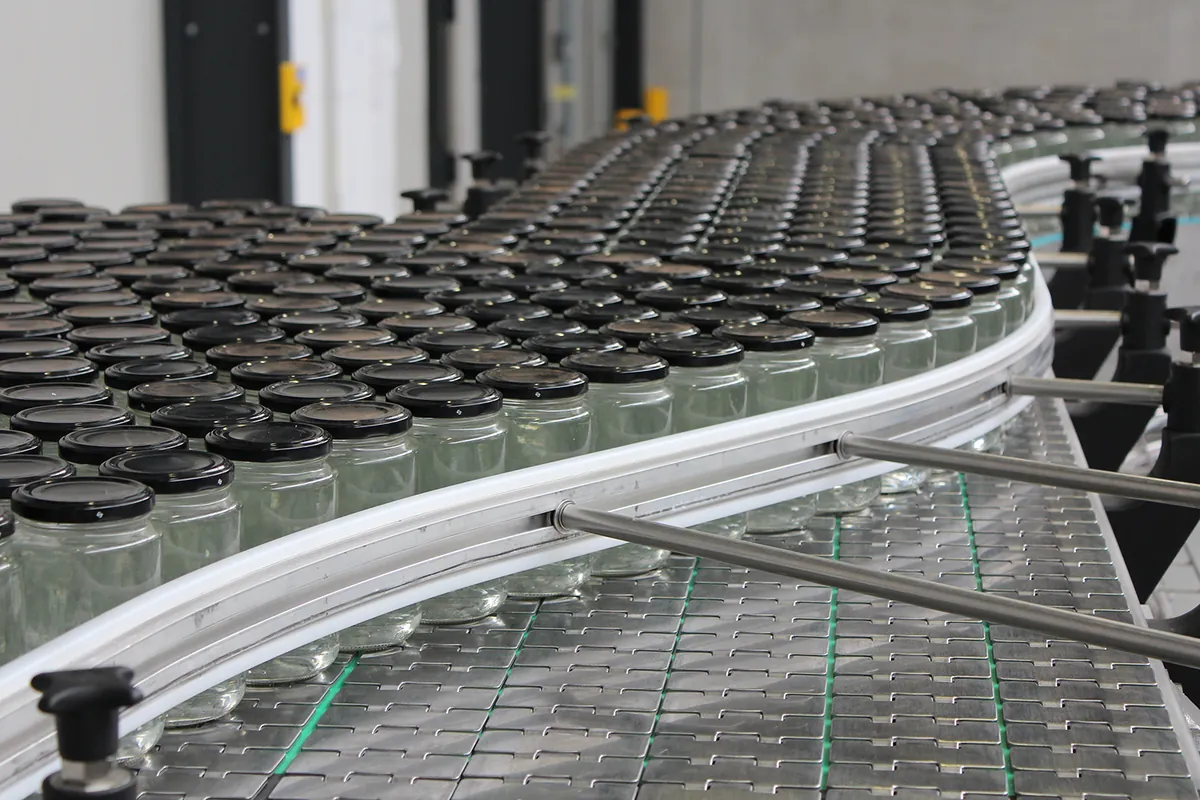
Conveyor guiding glass jars along a curved transport section
01

Designed around your product

Each conveying system is engineered to match the size, weight, surface, and behaviour of your specific products, ensuring stable and efficient transport.
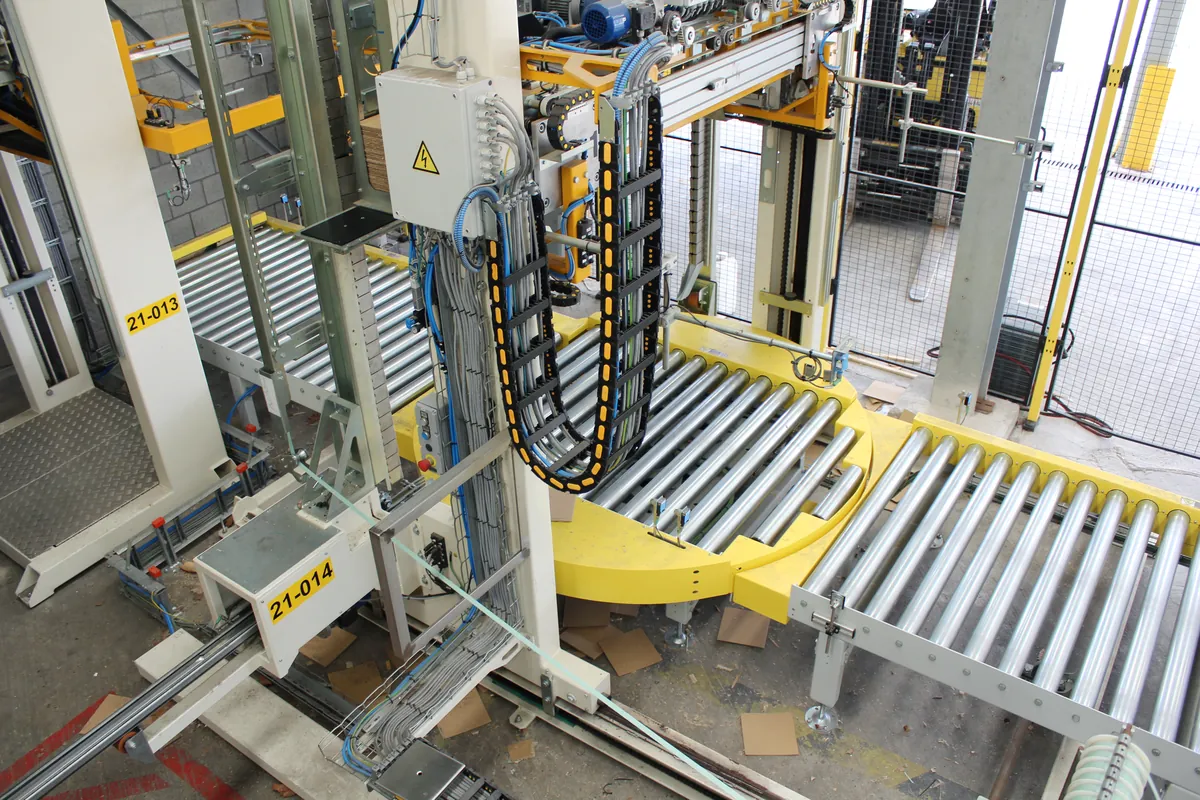
Roller conveyors and a turntable feeding drums into a robot cell
02

Seamless system integration

Conveyors are designed to connect seamlessly with machines, robotic handling, palletising systems, and production cells.
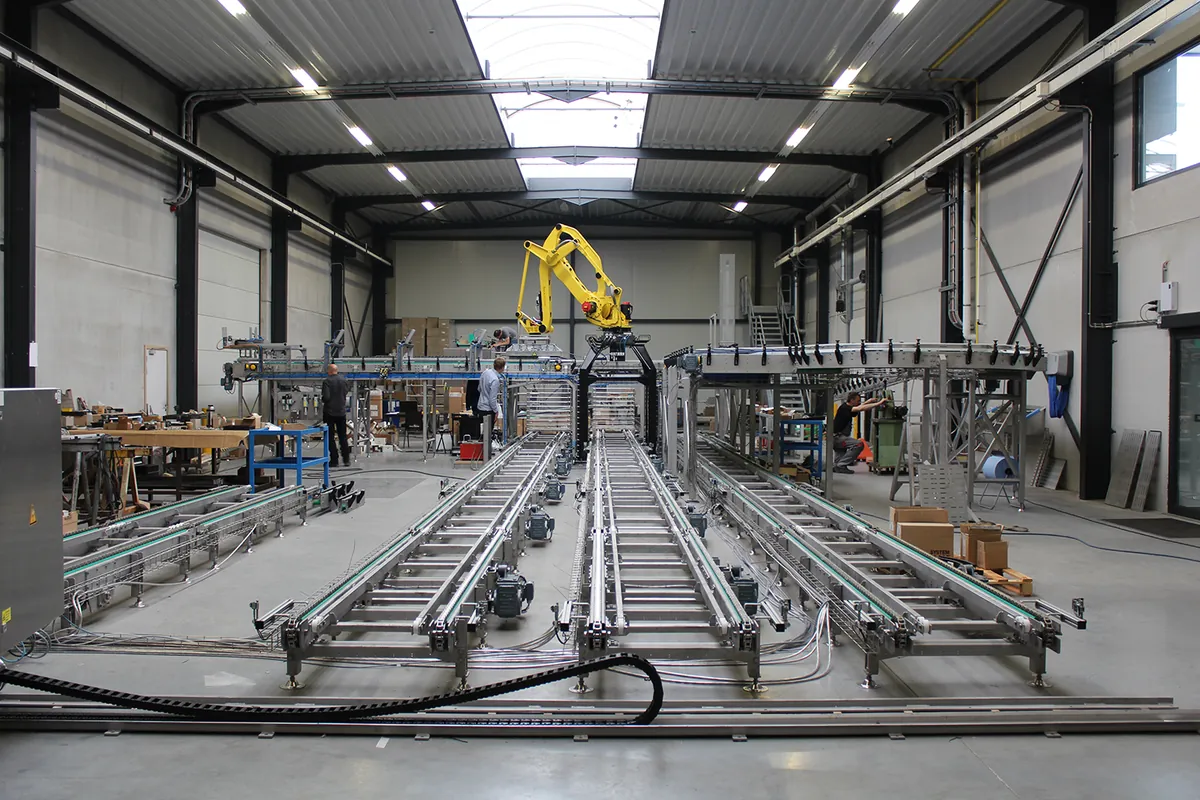
Long conveyor system running through a production hall
03

Built for continuous operation

Our conveying solutions are engineered for reliability, safety, and long-term performance in demanding industrial environments.
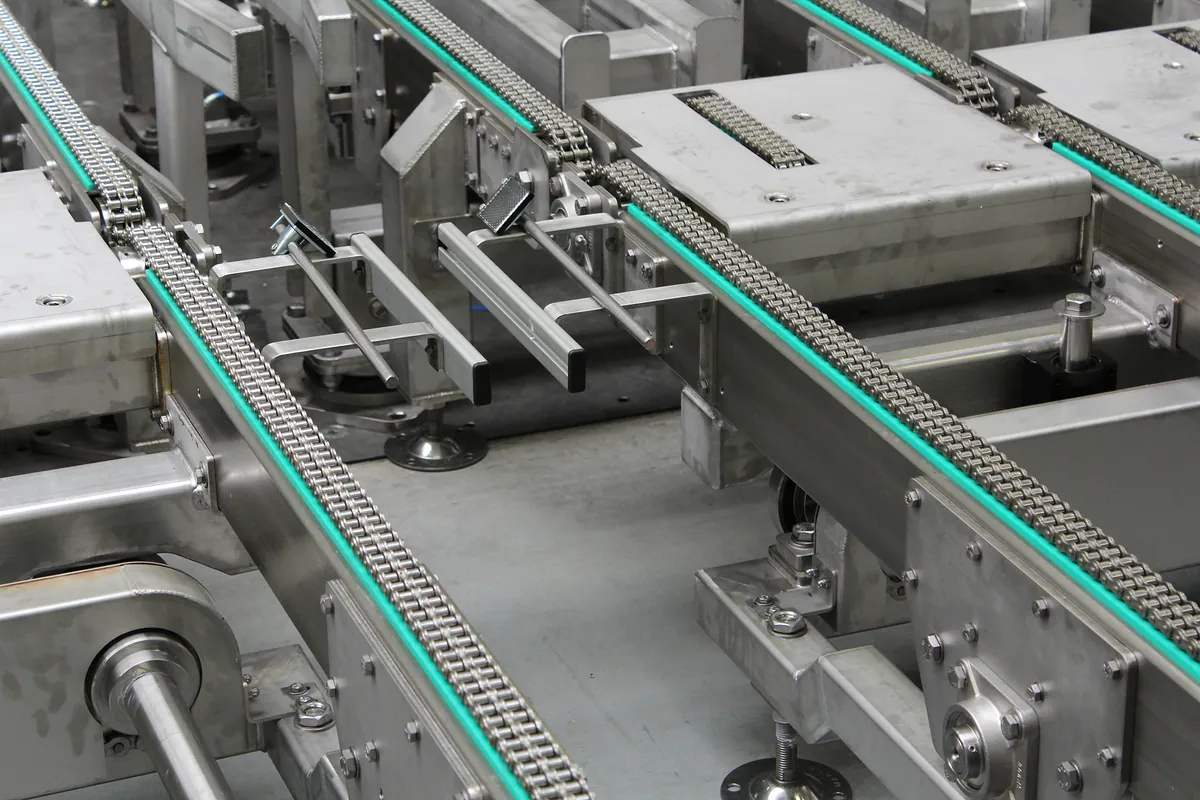
Modular chain conveyor sections ready to be extended
04

Flexible and scalable by design

Systems are designed to support future capacity increases, layout changes, or process adjustments without rebuilding from scratch.
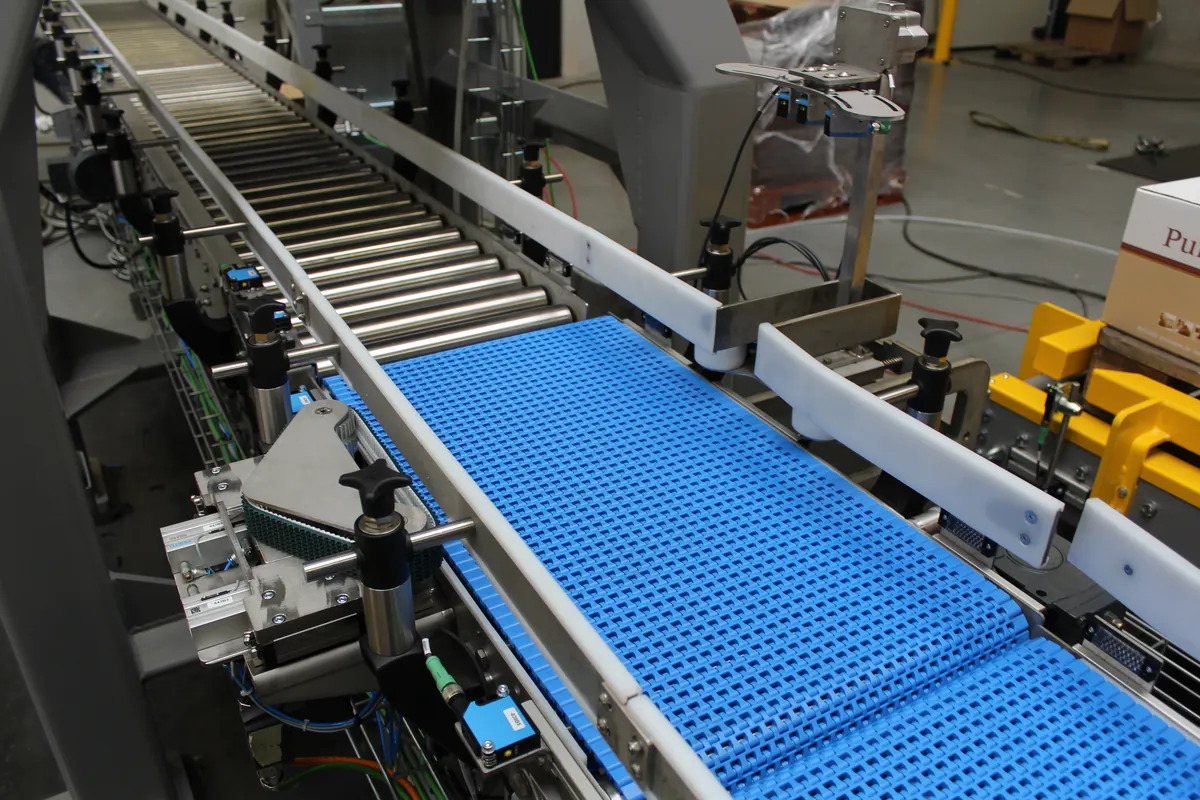
Conveying solutions for real production environments

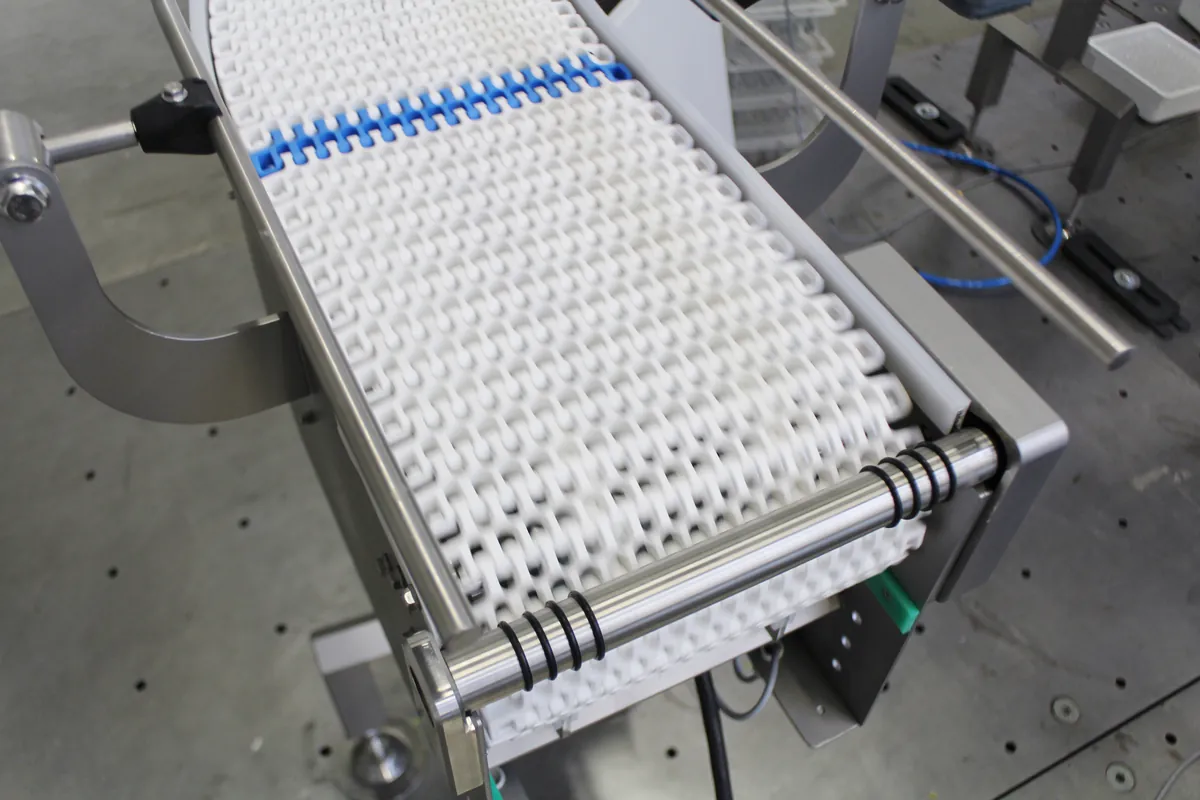
Belt conveyor with a blue modular belt

Belt conveyors

Versatile conveyors for a wide range of products and production needs.

  • Multiple belt material options
  • Adapted to product surface and handling requirements
  • Smooth and continuous transport
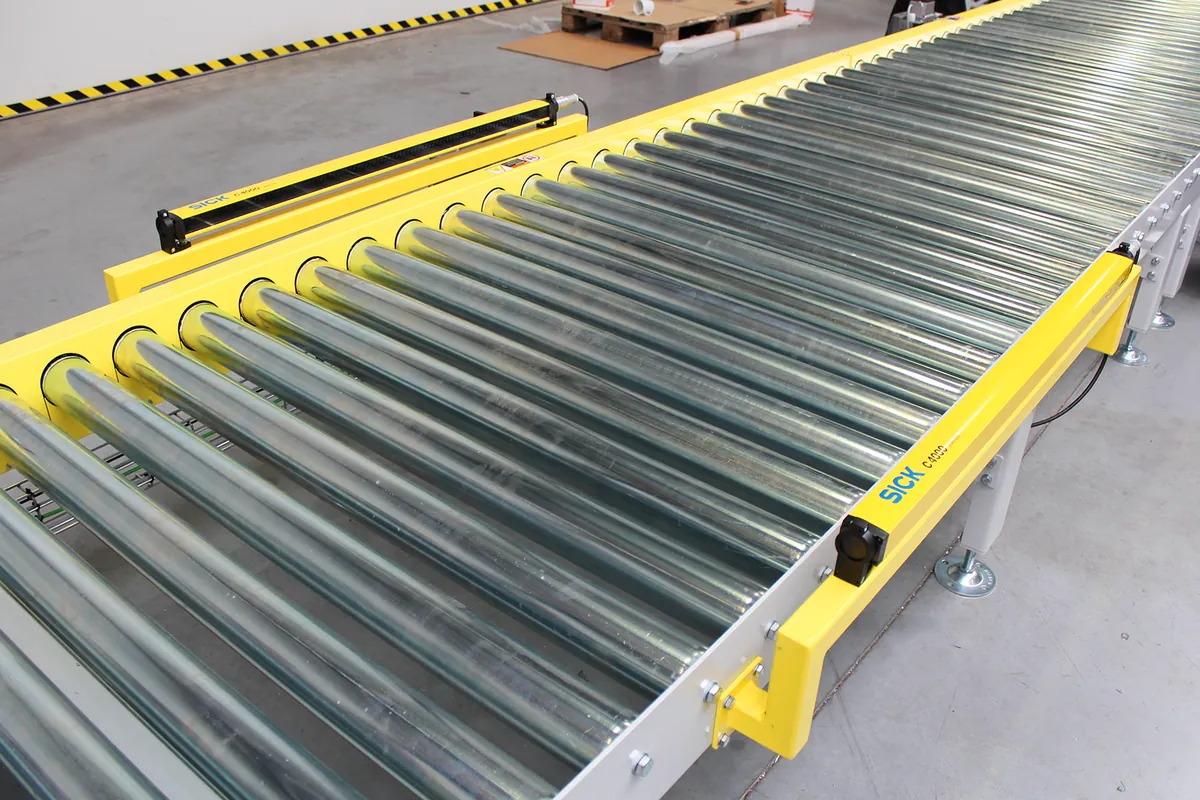
Roller conveyor for boxes and pallets

Roller conveyors

Reliable transport and buffering for packaged goods and pallets.

  • Ideal for crates, boxes, and pallets
  • Suitable for heavy loads
  • Commonly used in production and warehousing
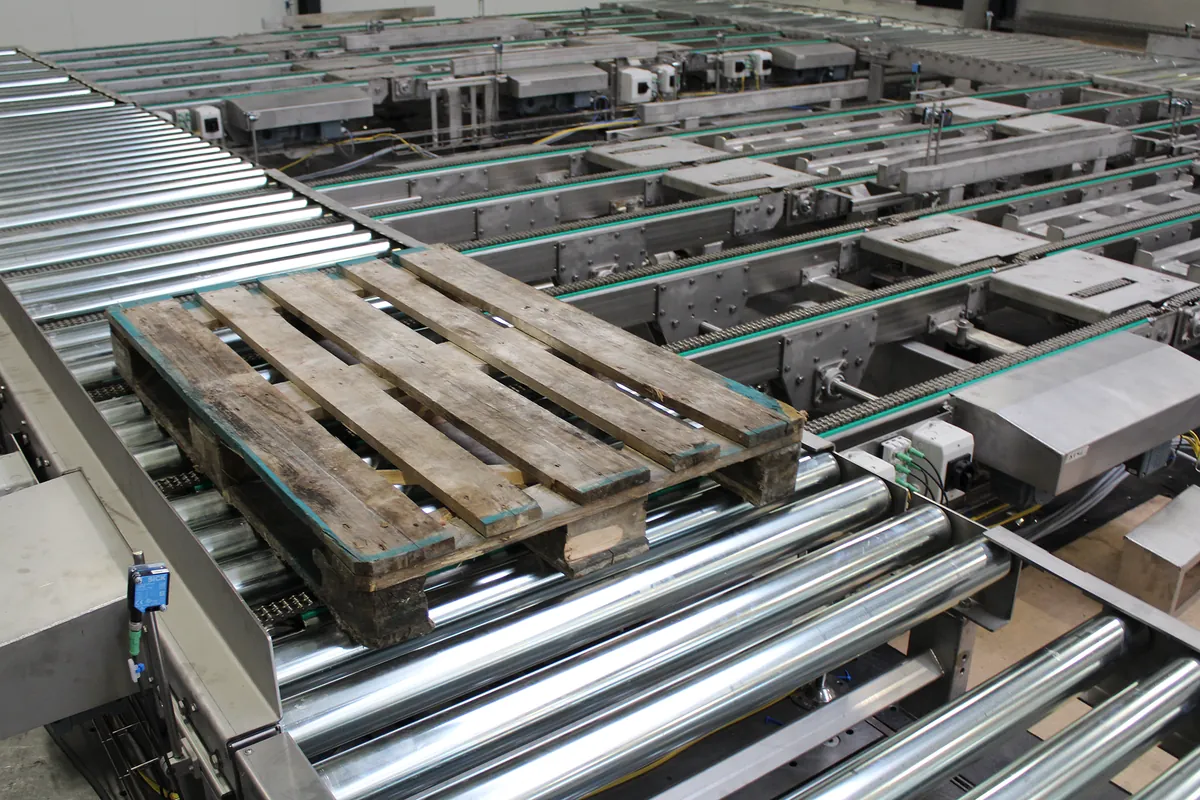
Chain conveyor transporting a wooden pallet

Chain conveyors

Rugged conveyors for demanding industrial applications.

  • Designed for pallets and industrial containers
  • Durable construction for harsh environments
  • Stable transport of heavy products
Conveyor with a rigid slatted conveying surface

Slat conveyors

Conveying solutions for heavy, hot, or challenging products.

  • Rigid and flat conveying surface
  • Suitable for extreme conditions
  • High durability and stability
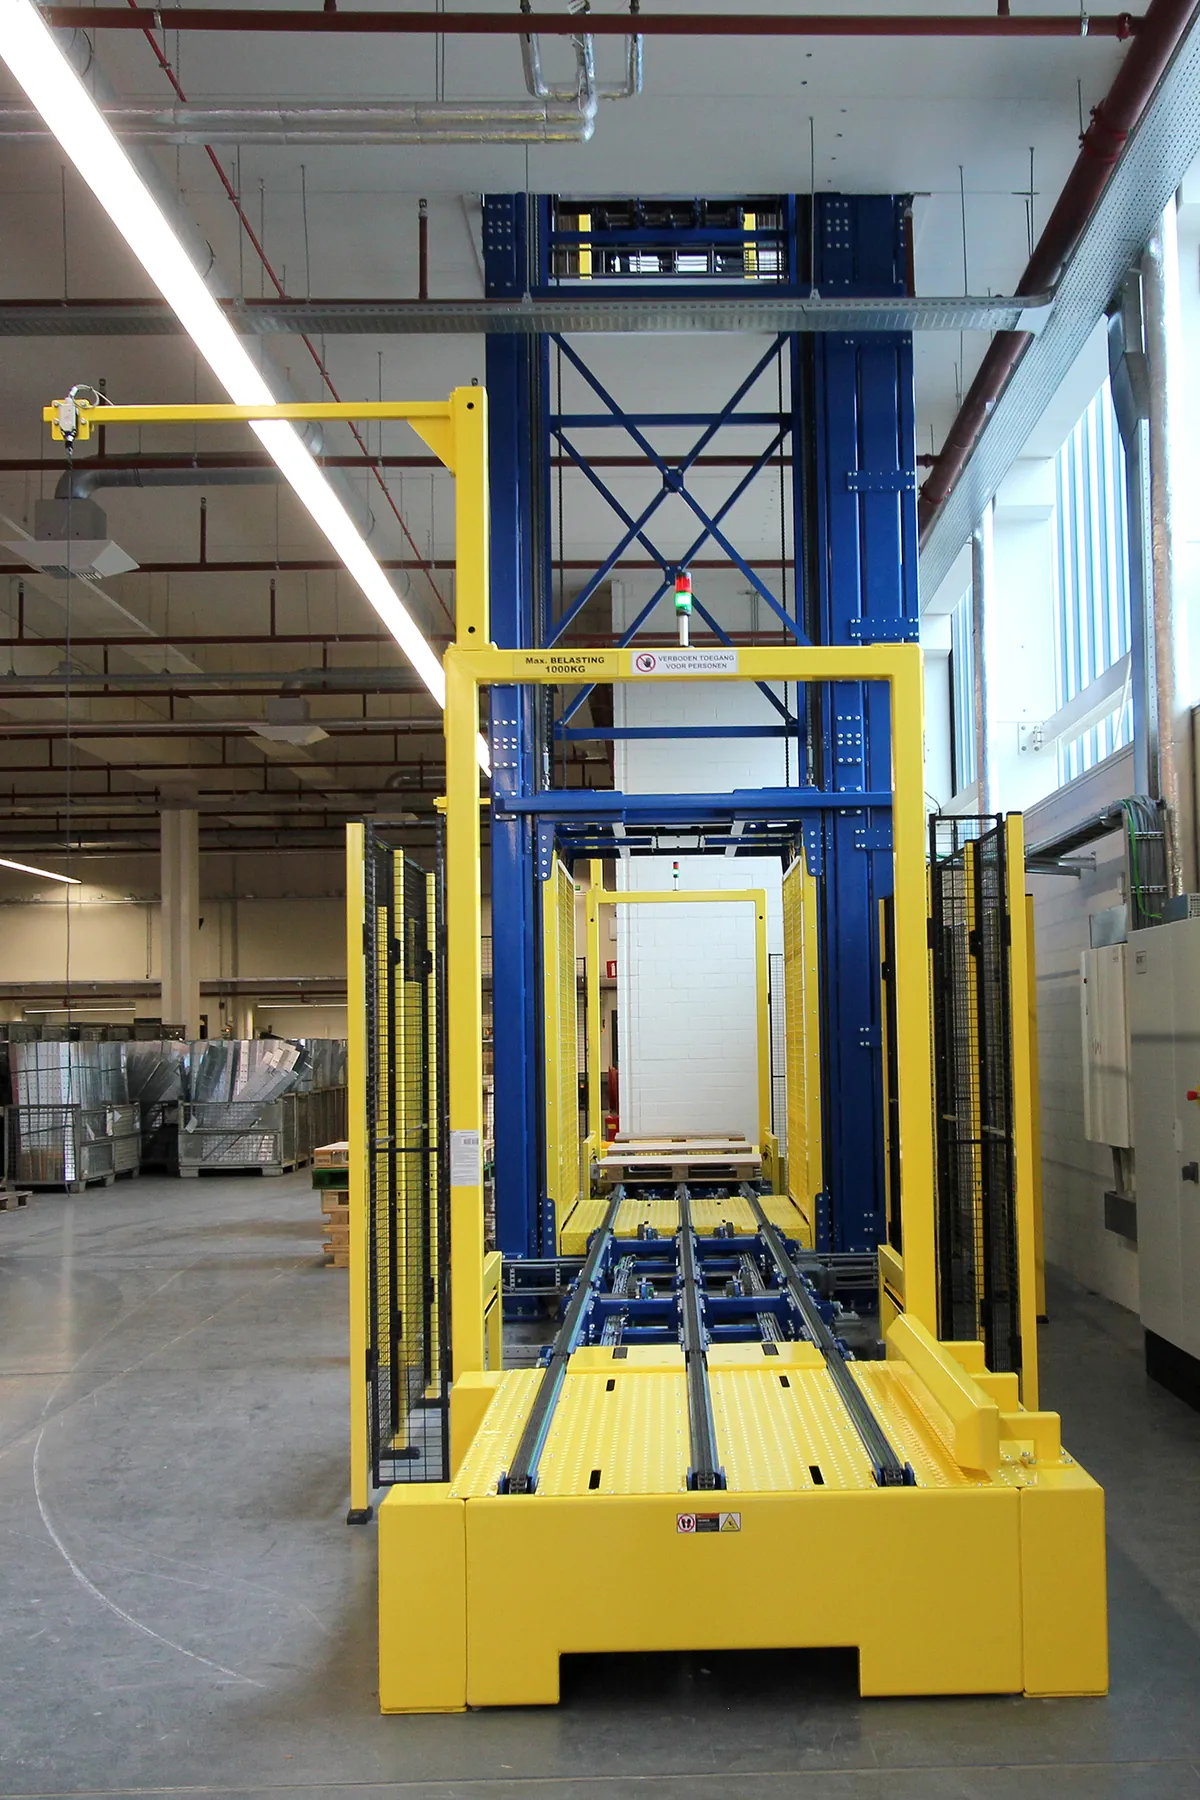
Pallet lift for transport between production levels

Auxiliary conveying equipment

Systems that support direction changes, elevation, and line transfer.

  • Turntables for direction changes and pallet handling
  • Pallet lifts for multi-level transport
  • Transfer cars for switching between lines

    In production

    Continental Foods

    Automatic loading and unloading of autoclaves

    Frequently asked questions

    What types of products can conveying systems handle?

    Conveying systems can be engineered to transport a wide range of products, including pallets, packaging, bulk materials, and fragile goods. Each system is designed around product dimensions, weight, surface, and handling requirements to ensure safe and efficient transport.

    Are conveying systems custom-designed or standard solutions?

    Conveying systems are custom-designed to match the specific production environment, product characteristics, and process flow. This ensures seamless integration with machines, robots, and production cells while optimising efficiency and reliability.

    Can conveying systems be integrated with robots and automation?

    Yes. Conveying systems are often integrated with robotic handling, palletising, and automated production cells. This creates a coordinated material flow that improves throughput and reduces manual intervention across the production line.

    Are conveying systems scalable as production grows?

    Conveying systems are designed with future expansion in mind. Capacity increases, layout changes, or additional equipment can be integrated without requiring a complete redesign of the system.

    Let’s design a conveying system that fits your production

    Tell us about your product, layout, and production goals. We’ll design a conveying solution that integrates seamlessly into your operation and supports efficient, reliable material flow.